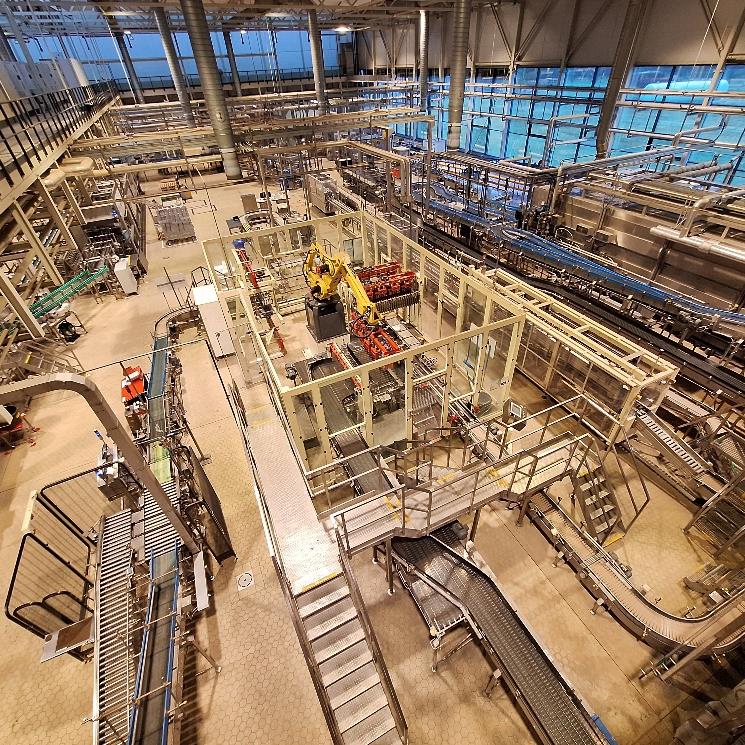
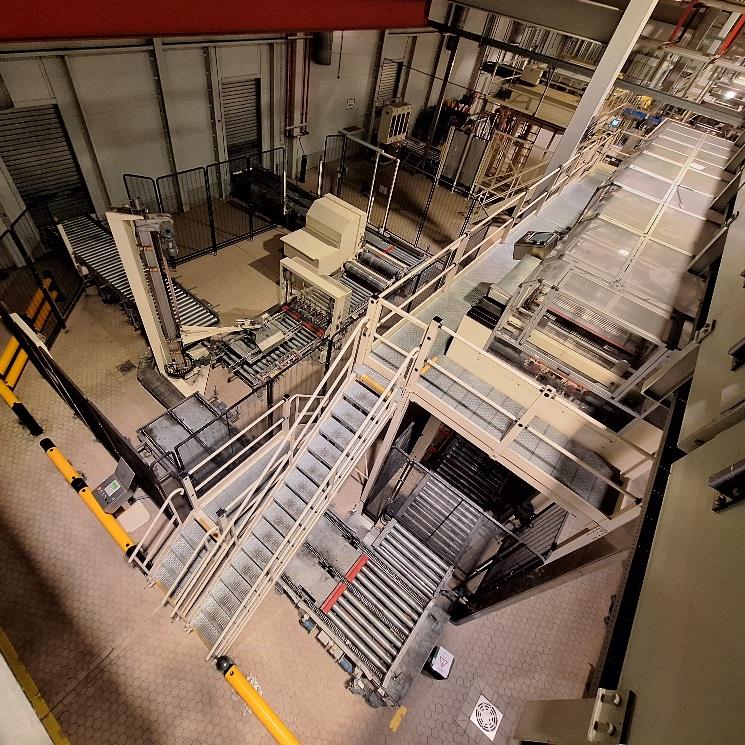
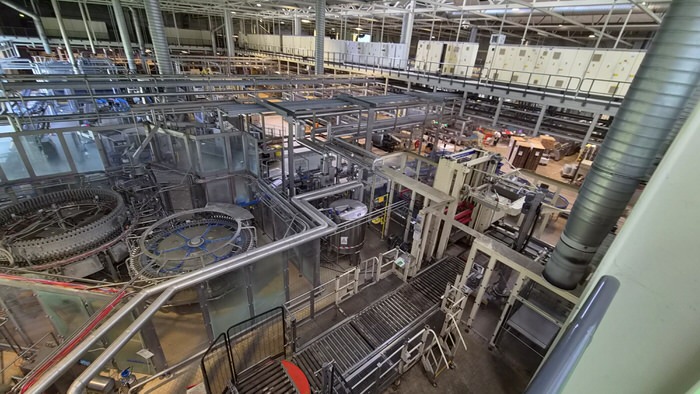
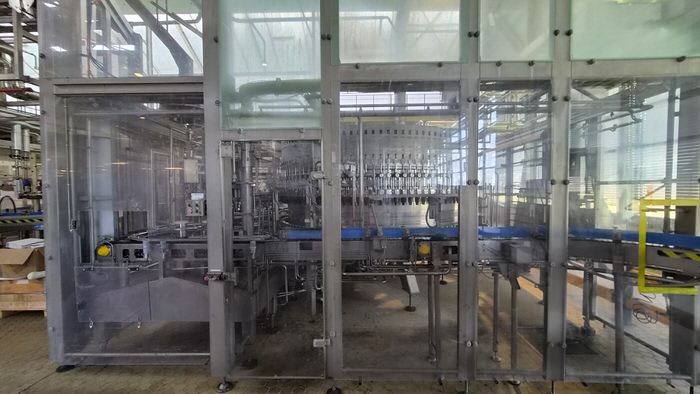
Non-Returnable Bottle (NRB) Packaging Line

Location: Netherlands
Available: Immediately
Key Specifications
Nominal speed in bottles per hour
- 25cl: 40.000/hr
- 33cl: 35.000/hr
- 50cl: 30.000/hr
Type of bottles
- 25cl, 30cl, 33cl, 50cl
Type of packaging
- 4 x 6 x 25cl
- 1 x 12 x 25cl
- 24 x 25cl
- 24 x 30cl
- 4 x 6 x 33cl
- 6 x 4 x 33cl
- 1 x 12 x 33cl
- 24 x 33cl
- 20 x 50cl
The nominal output (speed) of the individual machines are specified in the documentation and/or specifications of each machine. The line is designed for running in 3-shift operation at nominal speed, up to 7 days per week.

Key Characteristics
Production line is designed with the following characteristics.
- Transparent ‘See Through’ design
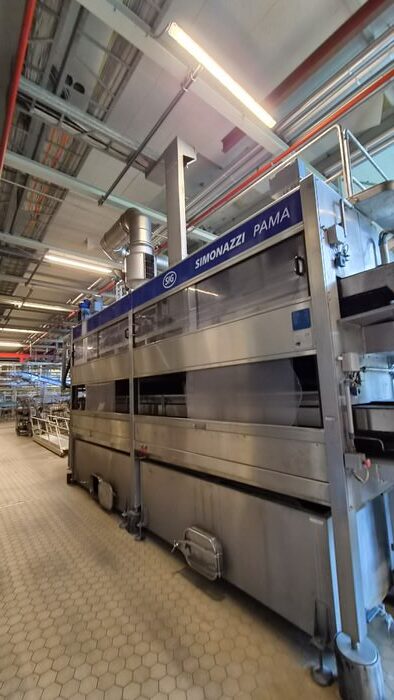
- World class machinery (SIG Simonazzi, Sidel, Logopak, Krones, Heuft, FANUC, Domino, Bortolin, BBULL, )
- Hygienic design
- Automatic grease lubrication of machines
- Automatic CIP
- Automated change-over
- Condition monitoring
- SCADA and MIS (Packaging Line Performance, Planning, Production and Downtime, Energy Consumption)
Processing of
Bottles
- Rinsing bottles with water
- Filling bottles with beer
- Capping bottles with crown caps
- Pasteurising beer in bottles
- Labelling bottles (neck, body, and back)
- Coding bottles
Packaging
- Unfolding
- Packing with beer bottles
- Coding
- Weighing
- Stacking on output pallet
- Shrinking plastic cover around output pallet
Production programmes
- All bottles arrive on bulk pallet 1200 * 1000 mm. The bottles are stacked on layer pads, which are reused. On top a carton tray is The bottles on the pallet are secured with shrink foil wrapping, which is removed manually before depalletising.
- The depalletised bottles enter a rinser/filler
- The bottles are rinsed and filled in a filler/crowner, flushed with water and inspected for fill height
- Products can be tunnel pasteurised or plate
- Before the labeller the bottles are blown off by an “air ”
- Next step is labelling, laser marking and label-/fill height- and leakage
- After labelling the bottles can travel in one direction to a carton packer
- The cartons are erected in a carton
- After erection, baskets are inserted into the
- Hereafter bottles are packed into the
- The cartons are closed and code
- 12 or 24 cartons are travelling via a full goods inspector directly to palletising.
- Empty pallets are inspected before entering the
- Palletised pallets are equipped with heat shrink plastic foil at top and sides
- Labels are supplied on the short and the long